Because cutting, machining, heat treatment, grinding and inspection all happen in our own facility, we control quality at each stage instead of chasing job workers.
Certified EN8, EN9, EN19, C45 and forged billets are sourced with mill test certificates and heat number traceability.
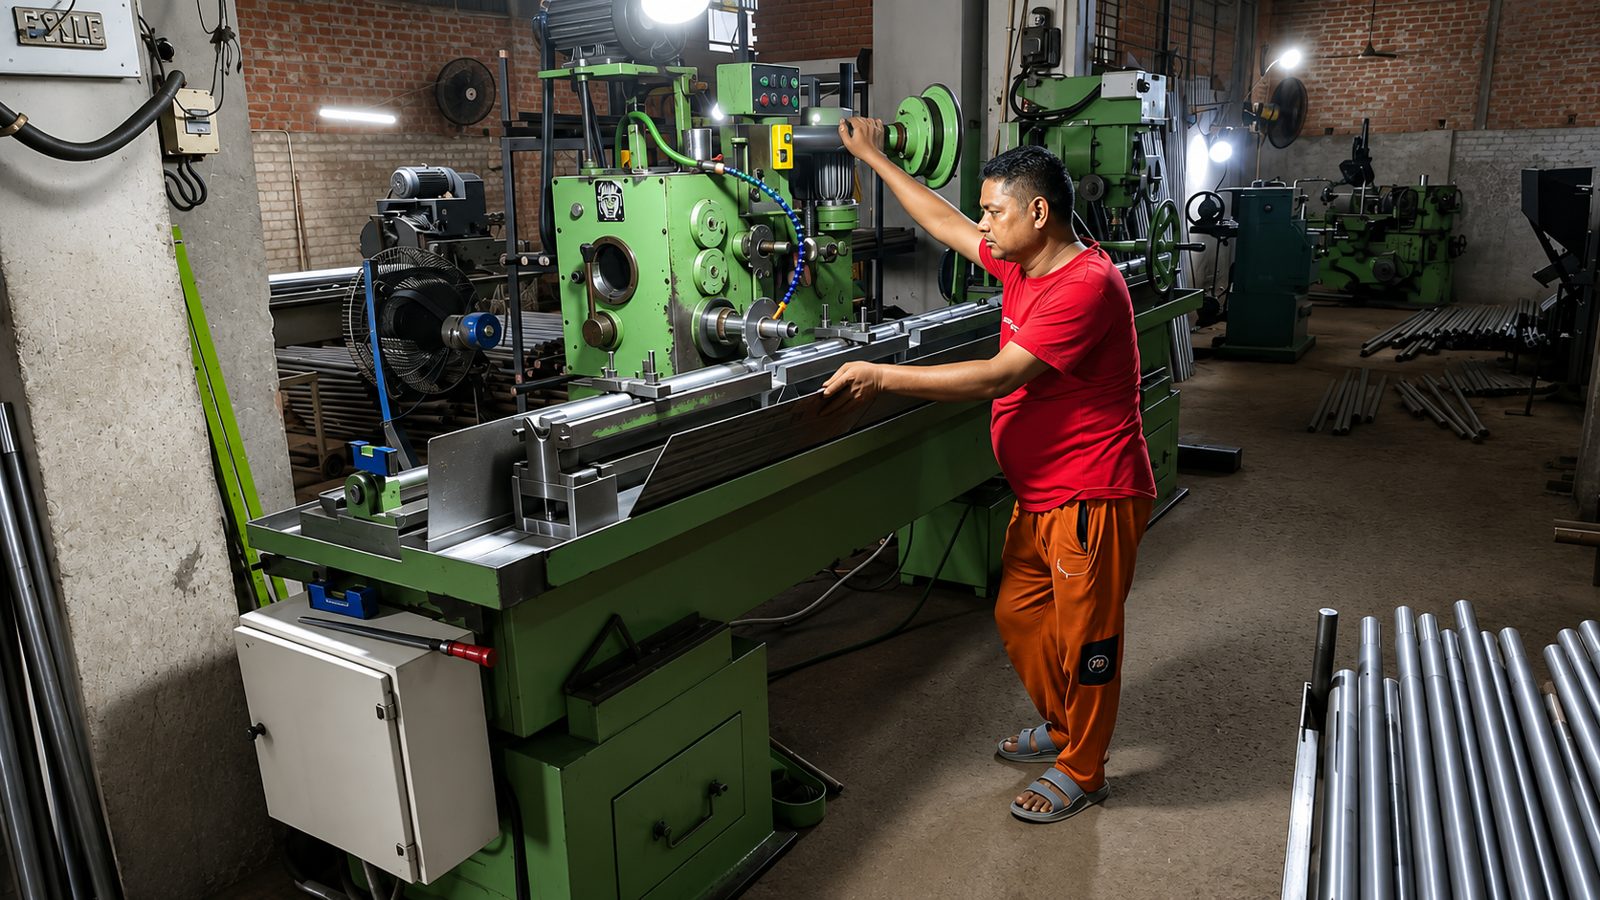
Bars are cut to length on bandsaws, then faced and centred so every subsequent operation runs true.
Diameters, steps, tapers and cam profiles are turned on CNC lathes against the approved drawing.
Keyways, slots, flats and cross holes are machined on milling centres with fixture-based repeatability.
Components are hardened and tempered to the specified hardness range, then hardness tested batch by batch.
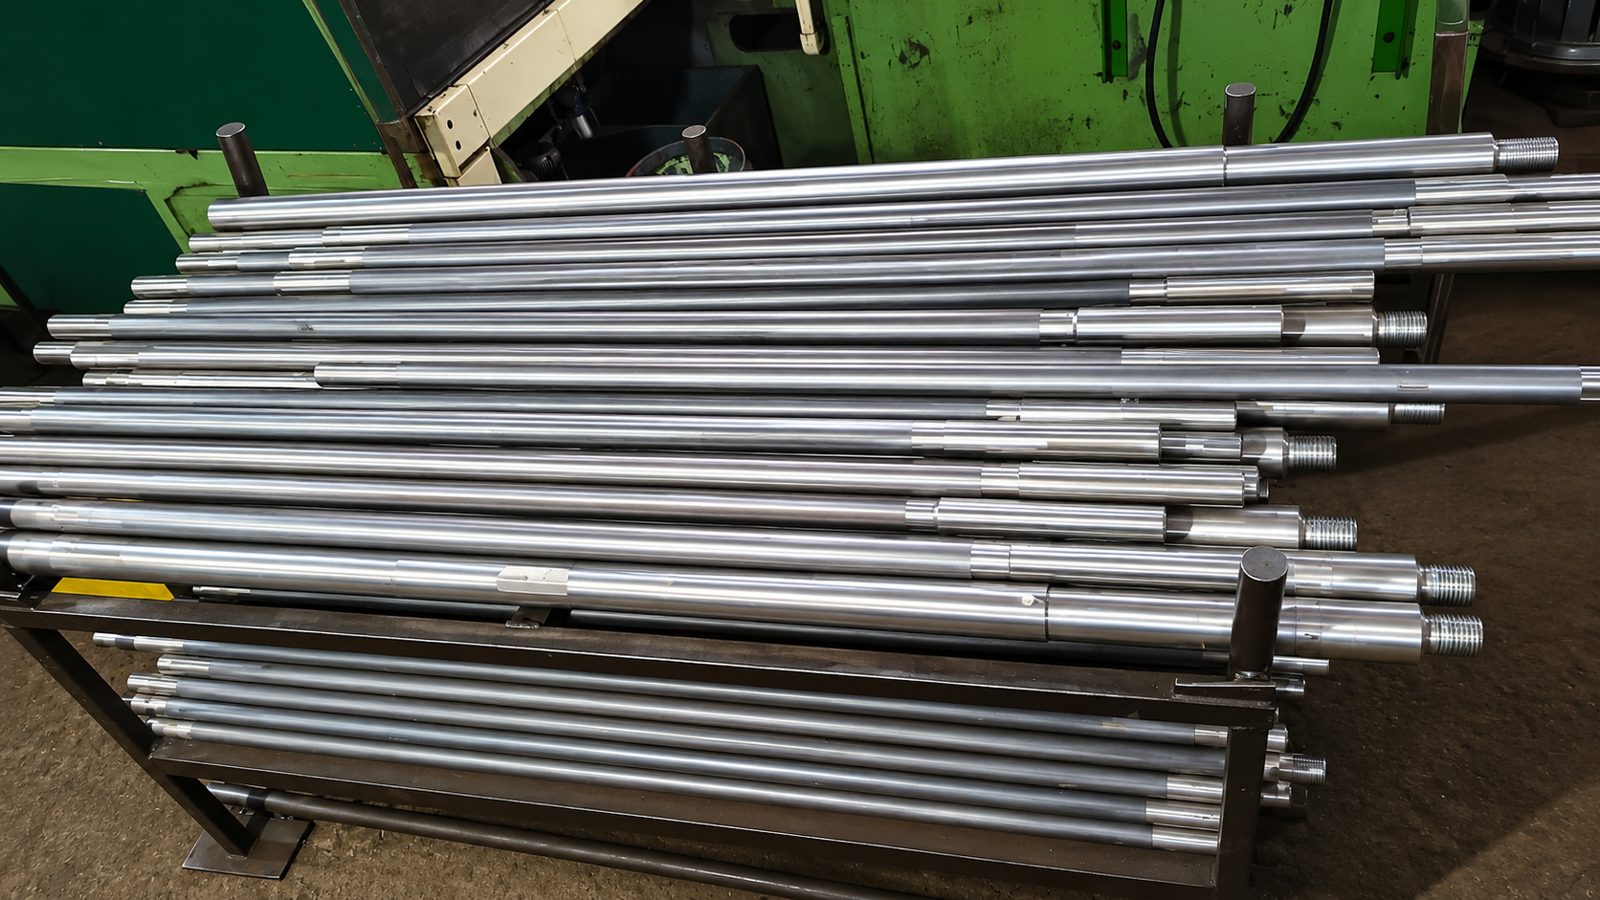
Bearing seats and critical diameters are cylindrically ground for tolerance, finish and low runout.
Gears and sprockets are hobbed or shaped to the required module and tooth count.
Sleeves, collars and gula bodies are pressed, welded and machined into ready-to-fit assemblies.
Dimensions, straightness, runout and thread fitment are checked with gauges, micrometers and dial indicators.
Parts are painted or powder coated, anti-rust treated and packed with edge protection for safe transit.
| Material verification | Mill test certificate and heat number recorded per lot |
|---|---|
| Dimensional check | Micrometers, vernier calipers and go/no-go gauges |
| Runout & straightness | Checked between centres with dial indicators |
| Hardness | Tested after heat treatment on every batch |
| Thread fitment | Verified with matching ring and plug gauges |
| Final audit | Visual and dimensional audit before packing |
Send it across with your quantity and we will confirm feasibility, price and delivery.